Posts

Showing posts with the label wps/wpqr/wqr

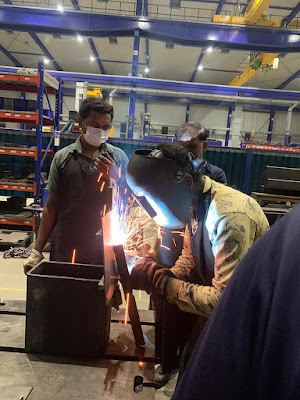
Welder Qualification at Messer Industries, Coimbatore

Image
  we provide  standard specifications for welding inspection procedures  for all welding process and Brazing. We offer Welder Procedure Specification, Welder Certificate Renewal Process, Procedure Qualification Record, Welder Qualification Testing, welder Training and Welder qualification services  in Coimbatore, Trichy, Salem, Erode, Chennai.

WELDING INSPECTION DUTIES

Image
  Welding Inspection duties General   Conditions:    Understand shop drawings, erection drawings, referenced codes and standards. Review the manufacturer’s  Material Test Report (MTR) . Verify all materials properties and that all materials are readily identifiable and traceable to an MTR.    Conduct a complete visual examination of the welding area for visible discontinuities. Visual examination should include, as a minimum, the finished conditions of the seam weld.    For visual examination, the only equipment commonly used is a  magnifying glass  (10x or less) and a  flashlight . Other tools, such as a  borescope and dental mirrors , are useful for inspection inside vessels, pipe, or confined areas.    For structural plates, piping, wrought and cast steel, conduct a complete visual examination of surfaces for visible fabrication defects or discontinuities.    Verify that all applicable welders, weldi...
Material Testing

Image
  Material testing Mechanical testing  have been designed to test several weld properties.Few other material testing techniques are Charpy V-Notch Toughness: Notch toughness is the capacity that a material possesses to  absorb energy  in the  presence of a flaw , such as a notch or crack. The material will likely exhibit a lower level of toughness. When a flaw is present in a material, loading induces a triaxial tension stres s state adjacent to the flaw. The material  develops plastic strains  as the yield stress is exceeded, near the crack tip. Notch-toughness is  measured with a variety of specimens  such as the  Charpy V-notch impact  specimen or the dynamic tear test specimen. As with regular impact testing the tests are often repeated numerous times with specimens tested at a different temperature. With these specimens and by varying the loading speed and the temperature, it is possible to  generate curves such as those s...

Dissimilar metal in TIG Welding process

Image
  Why use this TIG welding process: TIG Tungsten Inert Gas otherwise called as GTAW- Gas Tungsten Arc Welding , Involves melting the metal using the arc created by tungsten electrode, The welding can be done with or without filler metal, Argon Gas is used as shielding around the weld area, to shield the weld from atmospheric gases. As an inert gas is used for shielding the weld, the quality of weld is good without any Slag inclusions and good weld profile. TIG welding is selected to receive a high quality welds for analysis purposes   Where we use dissimilar metals ? Dissimilar metals are used in process pipe line industry, heat exchangers, boilers and Structural steel fabrication industry. SS 304/ SS316 (Austenitic Stainless Steel ) ASTM A -210  (Medium Carbon Steel) ASTM  A-36  (Low Carbon Steel )   Types of Weld Joint : Butt Joint, T Joint, Lap Joint , Corner Joint, Edge Joint Types of Joint Configuration: Joint Design:   Why we use Butt Joints To c...

Concepts of Welding Defects and Discontinuities

Image
   Welding defects can be classified as structural discontinuities and consist of: porosity, slag inclusions, lack of fusion, cracks, etc. Porosity  is gas pockets or voids in the weld metal which are free of any solid materials, such as It is formed as a result of gases driven from the weld metal, excessive currents, excessive arc lengths, and improper preparation of the joint. Porosity is generally classified into different groups as follows:  scattered, clustered and linear .    Scattered porosity occurs throughout the weld metal and the voids may vary in size from microscopic to slightly over 1/8 in.(3 mm). (Figure 6, below);    Clustered porosity occurs in groups and may generally be associated with a change in welding conditions. (Figure 7, below);    Linear porosity occurs throughout the length of a weld and the voids are in a line with respect to the axis of the weld. This type of porosity generally comes in the root pass and usu...

WELDING ELECTRODES AND PREHEAT REQUIREMENTS

Image
  The procedure requirements for welding electrodes and preheating temperatures are as follows: Welding must be done with the same process (SMAW or FCAW) used for qualification If the operator has qualified on any of the steel permitted (ASTM A36 and A588), that same operator is qualified to weld on the other and on SAE 1010 or ASTM. A welder qualified for manual shielded metal-arc welding with an  E7018  electrodes may also weld with  E7016 electrodes .Identifying electrode numbers are as follows:  a. The  70 designation  shall be understood to mean the  70 series  unless an alloy steel of higher strength is to be welded. b. The third digit indicates the position permitted. If the  digit is “1,”  the electrode may be used for welding in any position. If “2,” only the down hand position may be used. c. The  fourth digit  indicates the chemical make-up of the electrode coating. The  digit 6  indicates  low hy...

Recommendations for Welding

Image
  We would see about Recommendations for Welding of Structural Steel as per AWS D1.1 , 2020 revision Groove Weld: (Clause 4.4.1) Weld Length : shall be the width of the parts joined , perpendicular to the direction of compressive or tensile stress, Weld Size:  Thickness of thinner part of two joining sections, (with no excess re-enforcement achieved with a improper weld bead) Partial Penetration Weld : Weld Thickness: (Clause: 4.4.1.3) The size of Partial Penetration Groove welds shall be selected from the below  table 5.5  based on the thickness ‘ T’ of the joining base metal , Consider the thickness of the thicker part if two different thickness is joined. Fillet Weld Size. Minimum size of Fillet: (Clause :4.4.2.8) The minimum Throat thickness of fillet weld shall be selected from table below Size of Fillet Weld in Lap Joints: For Base Metal Thickness < 6mm , the fillet Leg size = thickness of base metal For Base Metal Thickness  >  6mm, the Fillet ...

Welding Standards-Positions for Welding Pipe

Image
  Positions for Welding Pipe For welding pipe in shops, power plants, oil refineries, and chemical plants for crude oil, gasoline, and natural gas, the same basic welding positions described previously are used. Flat Butt Weld Pipe Position – 1G A pipe to be welded in the flat position  is usually placed on roller dollies or wooden skids . As the pipe is welded, it’s rotated on the dollies or skids. This procedure  is the same as the flat position plate welding . The speed of rotation should be the same as the welder’s forward welding speed. Horizontal Butt Weld Pipe Position – 2G In this position, the weld around the vertical pipe  is the same of a horizontal position plate welding.  There is little difference whether the pipe is rotated or fixed because the welding is the same. Either the welder will circle around the joint, or the pipe itself can be turned in a circle if it’s free to rotate. Multiple Butt Weld Pipe Position – 5G In this position, the axis of ...